
Your Cart is Empty




Drag Chain Conveyor
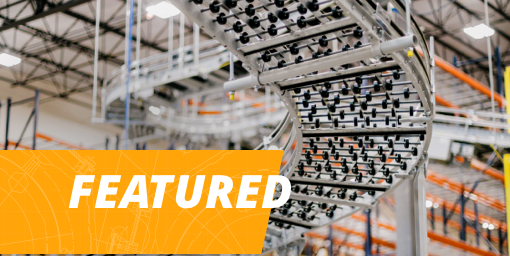
A spiral cooling conveyor holds product in moving air on a helical belt path so it reaches target temperature in transit instead of sitting on racks. Cooling, freezing, and proofing applications use spiral conveyors routinely because the long belt path inside a small footprint gives the product the dwell time it needs. The engineering problem is not vertical travel. It is buying enough minutes in the airstream without giving up floor space or throughput.
Dwell Time Is the Design Variable
On a transport spiral, belt speed is set by throughput. On a spiral cooler, belt speed is set by the dwell the product requires, and throughput becomes a function of belt width and product pitch.
The arithmetic is simple and it drives the whole spec:
Dwell equals belt length divided by belt speed. A 1,200 ft belt at 40 FPM delivers 30 minutes in the airstream. The same 1,200 ft belt at 100 FPM delivers 12 minutes.
Throughput equals belt speed divided by product pitch, times lanes. At 40 FPM with product on 12 in centers, one lane carries 40 pieces per minute. Three lanes carry 120.
Most transport spirals run between 100 and 200 feet per minute. A cooling spiral usually runs well below that, which is why the belt length, tier count, and enclosure get sized around the cooling curve rather than the conveyor catalog.
Cooling Rates FSIS Requires
For cooked meat and poultry, the cooling rate is a regulatory performance standard, not a preference. Fully cooked poultry products must be produced so there is no multiplication of toxigenic microorganisms such as Clostridium botulinum and no more than a 1 log10 multiplication of Clostridium perfringens within the product.
FSIS publishes cooling options that meet that standard in its Stabilization Guideline, commonly called Appendix B.
| Option | Cooling limits | Total |
|---|---|---|
| 1 (≤1.0 log10) | 130°F to 80°F within 1.5 hours; 80°F to 40°F within 5 hours | 6.5 hours |
| 2 (≤1.0 log10) | Chilling starts within 90 min of cook; 120°F to 80°F in 1 hour; 80°F to 55°F in 5 hours, then continuous to 40°F | 6 hours |
| 3 (≤1.0 log10) | Cured with ≥100 ppm ingoing sodium nitrite and 250 ppm erythorbate or ascorbate: 130°F to 80°F within 5 hours; 80°F to 45°F within 10 hours | 15 hours |
| 1 (≤2.0 log10) | 130°F to 80°F within 2.5 hours; 80°F to 40°F within 6.5 hours | 9 hours |
| 2 (≤2.0 log10) | 120°F to 80°F within 2.5 hours; 80°F to 55°F within 3.5 hours, then continuous to 40°F | 6 hours |
The 130°F to 80°F window is the tightest constraint in every option because it is the range of most rapid clostridia growth.
Continuous Cooling Beats Start-Stop Cooling
FSIS is explicit on this point. The cooling options apply to products that are cooled in a continuous manner and do not apply to processes where cooling starts and stops multiple times.
That distinction favors in-line cooling. A spiral cooler moves every unit through the same airflow for the same dwell, so the time-temperature profile is a process parameter you validate once and verify on an ongoing basis. Rack and cart cooling introduces variables FSIS names directly: product size, shape, and weight, plus stacking, storage, and how full the cooler is. A relatively empty cooler might not cool at the same rate as an overstuffed one.
Condensation Is the Hazard the Enclosure Creates
A spiral cooler is a tall enclosure with cold surfaces, moving air, and warm wet product underneath. That combination makes condensate, and condensate above exposed product is a contamination route.
Plants must be constructed so drip or condensate from fixtures, ducts, and pipes does not contaminate food, food-contact surfaces, or food-packaging materials.
FDA's Listeria guidance classifies conveyors as Zone 1 food contact surfaces and names fibrous and porous conveyor belts among potential sources of L. monocytogenes. It also recommends elevating conveyors above the floor to reduce splash and overspray, and avoiding overhead conveyors where practical.
Design the drip path before the spiral goes in: enclosure pitch, drip pans that drain away from the product zone, and tier spacing that keeps upper-tier condensate off lower-tier product.
Sanitary Construction for the Cooling Zone
Stainless steel construction, washdown-rated frames, smooth radius transitions, and Clean-In-Place compatibility are standard options on most modern spirals. The spec details, meaning belt material, drainage, and sensor placement, determine whether a unit passes the audit.
The Meat Institute's Food Safety Equipment Design Principles set the measurable criteria a cooling spiral gets reviewed against: product contact surfaces at Ra 32 µin or better, 304 or 316 stainless, hollow frames and rollers solid or sealed with continuous welds, no lap joints, and motors, gearboxes, and bearings kept out of and above the product zone. The same criteria govern any food grade conveyor feeding or discharging the spiral.
What Actually Gets Specified
Belt material and open area. Airflow has to reach the product, so belt open area is part of the cooling calculation, not just a belt choice.
Dwell plus exit temperature target. Give the integrator the entry temperature, the required exit temperature, and the time limit. Those three set belt length.
Airflow direction and volume. Counterflow air, air velocity, and refrigeration load are specified alongside the belt, not after it.
Enclosure and drainage. Washdown rating, drain locations, and access for cleaning and inspection.
Product handling. Whether product rides directly on the belt, on trays, or in containers changes the sanitary design entirely.
Controls and records. Speed control, temperature monitoring, and data capture that supports validation and ongoing verification.
Spiral Cooler, Spiral Freezer, or Cooling Tunnel
These solve different problems. A spiral cooler pulls product down to ambient or refrigerated temperature. A spiral freezer drives product through the freezing curve and carries a much larger refrigeration load and heavier insulation. A straight cooling tunnel is simpler and cheaper but consumes floor space in direct proportion to the dwell you need, which is the tradeoff spirals exist to avoid.
Putting a Spiral Cooler In With HOJ
Whether you are adding one spiral cooler or building the line around it, HOJ handles the whole scope with one team. You get one point of contact and one company accountable for whether the product hits temperature.
We spec to your cooling curve, not a vendor's catalog. HOJ is an authorized Hytrol Integration Partner and evaluates equipment from other proven manufacturers when the application calls for it, so the spiral gets chosen for your product.
Controls are built and tested before we arrive. HOJ's PLC and controls integration team builds UL 508A panels and writes the code in-house, then proves it in factory acceptance testing, so your line is down as briefly as possible.
Our own crews install it. HOJ installers include veterans with more than 20 years installing conveyor, and the work is reviewed by independent third-party engineers and safety inspectors.
The work is warrantied and serviced. Installation carries a one-year HOJ warranty plus manufacturer warranties on equipment, and HOJ services spirals with chain tensioning, slat inspection, drive and motor service, alignment audits, and locally stocked spare parts.
Tell us your entry temperature, target exit temperature, and throughput, and an HOJ engineer will size the spiral for your line.
Testimonials
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.