
Your Cart is Empty




Food Grade Conveyor
Food Grade Conveyor Solutions
Table Top Conveyor
What this does
Interlocking flat top plates carry bottles, cans, jars, and cartons single file through curves and elevation changes in one run. Stainless steel and friction-top plates suit bottling, food, and washdown lines.
Mat Top Conveyor
What this does
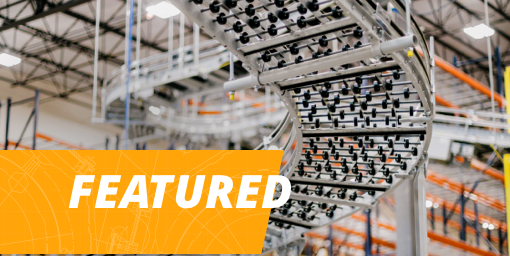
A wide modular plastic belt carries cases, trays, and packaged goods in mass flow around curves and spirals with no dead plates. Sanitary and washdown versions are built for food and beverage lines.
Plastic Chain Conveyor
What this does
A multiflex plastic chain on an aluminum beam bends horizontally and vertically to route jars, pouches, trays, and boxes up to about 30 kg through compact packaging and machine-tending cells.
Food Grade Conveyor
A food grade conveyor is built so every product contact surface, and every surface near or above the product zone, can be cleaned to a microbiological level and hold up to the sanitation chemistry used on it. FDA's current good manufacturing practice rule requires holding, conveying, and automated systems to be designed and constructed so they can be maintained in a clean and sanitary condition (21 CFR 117.40(d)). HOJ engineers food processing conveyor systems with the controls, washdown-rated electrical, and downstream packaging and pallet handling designed as one line.
The Regulatory Baseline for Food Processing Conveyor Systems
21 CFR 117.40 sets the floor for any conveyor in an FDA-regulated facility. Equipment must be:
- adequately cleanable and maintained against allergen cross-contact
- installed so the equipment and adjacent spaces can be cleaned
- built to keep lubricants, metal fragments, and contaminated water out of food
Food contact surfaces must be corrosion resistant, nontoxic, and able to withstand the product, cleaning compounds, and sanitizers. Seams on food contact surfaces must be smoothly bonded to limit buildup of food particles and microbial growth. Equipment that never touches food but sits in the processing area must still be constructed so it can be kept clean.
For meat and poultry, NSF/ANSI/3-A 14159-3 sets hygiene requirements specifically for mechanical belt conveyors handling exposed product.
Sanitary Conveyor Design Criteria
The Meat Institute's Food Safety Equipment Design Principles (2021) convert the cleanability requirement into measurable criteria. The principles were written for meat and poultry equipment, and the Meat Institute notes they may apply to other wet-cleaned food operations. Key criteria for a stainless steel sanitary conveyor:
| Design element | Criterion |
|---|---|
| Product contact surface finish | Ra 32 µin (0.81 µm) maximum |
| Non-product contact surface finish | Ra 125 µin maximum |
| Stainless steel | 304 or 316 grade, or equivalent |
| Internal corners under 135° | Continuous radius of 1/8 in minimum |
| Hollow frames, rollers, and pulleys | Solid, or sealed with continuous welds |
| Joints and welds | No lap joints; welds continuous, smooth, and polished |
| Fasteners | None in or above the product zone |
| Floor clearance | 12 in for the installation; 18 in for product contact surfaces and return paths |
| Overhead and wall clearance | 30 in from overhead structures; 36 in from walls and stationary objects |
| Motors, gearboxes, bearings | Not located in or above product contact zones |
The same checklist excludes painted, plated, and coated surfaces from food contact and from surfaces above the product zone. It also rules out caulking, press and shrink fits, barbed hose fittings, and cloth-back belts.
Harborage Points That Fail Environmental Monitoring
FDA's draft guidance on Control of Listeria monocytogenes in Ready-To-Eat Foods names conveyor rollers as equipment that should not be hollow or foam filled, because they collect water that harbors L. monocytogenes. The guidance classifies packaging equipment and conveyors as Zone 1 food contact surfaces. It also lists fibrous and porous conveyor belts among potential sources of the pathogen.
The guidance recommends:
- elevating conveyors above the floor to prevent splash and overspray
- keeping stationary equipment off floor drains
- avoiding overhead conveyors where practical
Where overhead runs cannot be avoided, they must be built so drip and condensate do not contaminate food or food contact surfaces. Existing equipment that does not meet these points should be modified, replaced, or placed on a documented cleaning schedule paired with environmental monitoring.
Food Grade Conveyor Belt and Material Selection
Plastics. Belt modules, wear strips, and guides must remain intact without changes in shape or function through operation, sanitation, and storage, and must comply with 21 CFR Parts 175 to 177. Polyethylene and polypropylene food contact components fall under 21 CFR 177.1520.
Metals. Stainless steel should be 304 or 316. Grade 316 adds 2 to 3 percent molybdenum for better pitting resistance where chlorides are present in brines, product, or sanitation chemistry. Metals in contact with one another must be compatible to prevent galvanic corrosion.
Excluded materials. Wood, enamelware, and uncoated or anodized aluminum are not acceptable under NSF/ANSI/3-A 14159-1.
Foreign material. FDA considers ready-to-eat food containing a hard or sharp foreign object 7 to 25 mm long to be adulterated. Fragments from chipped belt modules, scraper blades, and wear strips can fall in that range. The Meat Institute principles call for breakable or removable parts to be detectable, and metal-detectable belt and component compounds are one way to meet that criterion.
Washdown Conveyor Drives, Controls, and Enclosures
Drives and electrical components on a washdown conveyor carry their own sanitary design requirements. The Meat Institute principles:
- keep motors, gearboxes, and bearings out of and above the product zone
- keep push buttons and HMIs away from open product
- prohibit conduit runs above product contact areas
- require enclosures in direct washdown areas to withstand high-pressure washing
For hot, high-pressure sanitation, the relevant rating is IP69K, or IPX9 under IEC 60529. The test sprays 80 °C water at 8 to 10 MPa and 14 to 16 L/min from 100 to 150 mm. HOJ builds UL 508A control panels in-house, so enclosure ratings, panel locations, and cable routing are specified in the same design as the conveyor.
Lubricants and Compressed Air on Food Lines
21 CFR 178.3570 allows lubricants with incidental food contact on food handling machinery. They must be applied at the minimum amount needed, with mineral oil in food capped at 10 ppm. NSF registers compliant products as H1 lubricants.
Compressed air used on food or to clean food contact surfaces must be treated so it does not contaminate food (21 CFR 117.40(g)). The Meat Institute recommends filtered, dried air with 0.01 micron final filtration for product applications and pneumatic exhaust directed away from product contact surfaces.
Matching Sanitary Construction to the Plant Zone
Not every conveyor in a food plant handles exposed product. FDA's zone model treats food contact surfaces as Zone 1, and those surfaces run from processing and cooling through primary packaging.
Sealed packages, cases, and pallets downstream of the sealer present a different exposure. Those conveyors fall under the non-food-contact requirement of 117.40(c), which still requires construction that can be kept clean.
HOJ designs the full line by zone, from sanitary conveyor at exposed product through case conveyor, spiral conveyor, palletizing, and pallet handling, so each section is built to the standard its exposure requires.
Engineering and Service Through HOJ
HOJ integrates sanitary conveyor from manufacturers including Nercon and Intralox, with controls engineering, installation, and service handled by its own teams.
Principle 10 of the Meat Institute framework calls for written, validated cleaning and sanitizing protocols, and the equipment has to support them. That means tool-free belt tensioning, accessible bushings, sprockets, and bearings, and belt lifters where belts stay on the frame.
HOJ's 70+ vehicle service fleet supports food lines with belt and wear strip replacement, drive and bearing service, and alignment.
Testimonials
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.