
Your Cart is Empty




Sanitary Spiral Conveyor
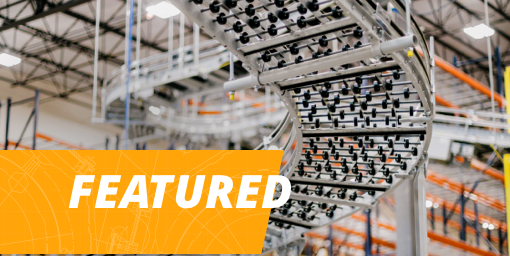
A sanitary spiral conveyor is built so every surface the product touches, and every surface above it, can be cleaned and verified clean. HOJ specifies washdown stainless spiral conveyors for food, beverage, and pharmaceutical lines, along with any operation that hoses down its equipment on a shift schedule.
The difficulty is geometric. A straight conveyor gives a crew an open bed and clear sightlines. A spiral gives them stacked tiers, a rotating column in the middle, and a return run buried inside the tower. Sanitary design on a spiral is the work of buying back the access the shape takes away.
What Sanitary Actually Means Here
Three things, and they are the same three whether you run yogurt, tablets, or shampoo.
Cleanable surfaces. Smooth finishes, continuous welds, radiused internal corners, and no seams or fasteners that trap residue.
Physical access. A crew can reach every surface without special tools, and reach it in the time the sanitation window allows.
Controlled drainage. Water and product go somewhere by design instead of pooling on a frame member or dripping onto the tier below.
Stainless construction, washdown-rated frames, smooth radius transitions, and Clean-In-Place compatibility are standard options on most modern spirals. The spec details, meaning belt material, drainage, and sensor placement, determine whether a unit passes inspection.
The Drum and the Rollers Decide the Build
This is the single highest-stakes decision on a sanitary spiral. Rotating components, including the drive drum, sprockets, support rollers, and belt pulleys, should be solid, or fully sealed with continuous welds where solid is not practical. Hollow tube construction does not belong at or above the product zone, and where it is used below, it needs continuous welds and no fastener penetrations.
The reason is water. FDA recommends that conveyor rollers not be hollow or foam filled, because they collect water that harbors pathogens, and existing equipment built that way should be modified, replaced, or put on a documented cleaning schedule with environmental monitoring behind it.
On a spiral this applies to a large central drum or cage plus every idler in the helix, which is a lot of rotating mass to seal. It is worth asking any manufacturer directly, in writing, before the order.
Designing Access Into a Helix
Access is not a feature you add to a spiral. It is a decision made in the frame design.
Belt lifting. The belt and rail system has to be reachable for cleaning and inspection, which on a tall spiral usually means lifters built into the machine rather than supplied loose.
Tool-free tension release. Tension should come off by hand so the crew can get to the bed. If the belt has to come out for periodic cleaning, there needs to be a defined place to put it.
Removable wear parts. Scrapers, rub bars, and belt supports should come off without tools, and scrapers should be single pieces mounted clear of the product drop zone.
Every one of these is cheap at design and expensive after installation.
Clearances Get Settled at Layout or Not at All
Spirals are tall, heavy, and usually dropped wherever the floor plan has room. Sanitary clearance requirements do not flex for that.
| Requirement | Clearance |
|---|---|
| Equipment to floor | 12 in |
| Product contact surfaces to floor, including return belt paths | 18 in |
| Clearance from overhead structures | 30 in |
| Clearance from walls and other fixed objects | 36 in |
The return path clause is the one that catches spirals. The belt comes back down inside or beneath the tower, that run is still a product contact surface, and it still owes 18 inches to the floor.
A spiral installed a foot off a wall cannot be corrected later without moving the machine. HOJ walks clearances during layout for exactly this reason.
Stacked Tiers and Where the Water Goes
Every tier sits above the one below it, so anything that pools or drips upstairs lands on product downstairs.
Surfaces should be self-draining, horizontal framework rounded or angled so nothing sits on it, and belts supported well enough that they do not sag and hold water. Drip pans are acceptable, but they have to drain away from the product zone and come out easily for cleaning.
The regulatory floor is the same idea. Facilities must be built so drip or condensate from fixtures, ducts, and pipes does not reach food, food contact surfaces, or packaging materials.
Chilled or enclosed spirals make this harder, because cold surfaces plus warm product generate condensate on their own.
Washdown Electrical Is Half the Job
The frame usually gets specified carefully and the electrical gets specified last, which is backwards for a machine that gets hosed down.
Motors, gearboxes, and bearings belong outside and below the product zone. Conduit does not run above product contact areas. Push buttons and operator screens sit away from open product.
For high-pressure, high-temperature cleaning the rating to ask for is IP69K. That test sprays 80 °C water at 8 to 10 MPa and 14 to 16 L/min from 100 to 150 mm, from four angles.
HOJ builds UL 508A panels in-house through its PLC and controls integration team, so enclosure ratings, panel locations, and cable routing are designed with the spiral instead of added to it afterward.
Materials Beyond the Default
Grade 304 stainless is the default. Grade 316 adds 2 to 3 percent molybdenum and resists pitting better wherever chlorides are present, which covers brines, many cleaning chemistries, and most sanitizers.
Dissimilar metals in contact invite galvanic corrosion, and painted, plated, or coated surfaces do not belong in or above the product zone.
The right grade is set by your sanitation chemistry, not by the product.
Where CIP Earns Its Keep
Clean-In-Place is the right answer when disassembly is genuinely impractical, and it comes with a condition people skip: you need a way to verify it worked.
Specifying CIP does not close the gap by itself. Spray coverage has to reach the surfaces disassembly would have reached, and you need swab points and a verification method that proves it did. Otherwise CIP is a claim, not a control.
Why Operations Bring HOJ In
A sanitary spiral is one of the few machines where a specification mistake cannot be corrected with a work order. Clearances, sealed rotating components, and drainage paths are decided once, at design, and everything after that is either compliant or a finding.
HOJ has engineered material handling since 1964, and we take the whole scope so nobody is left holding a gap.
We are not selling you one manufacturer's spiral. HOJ is an authorized Hytrol Integration Partner and evaluates other proven manufacturers when the application calls for it, so the machine gets matched to your product, your sanitation chemistry, and your cleaning window instead of to a line card.
The controls are ours, not a subcontractor's. Most integrators design the conveyor and hand the electrical to someone else. HOJ engineers controls in-house and builds UL 508A panels in our own shop with full schematics, BOM, and component traceability, which is why washdown ratings, panel placement, and cable routing get designed with the machine.
Our own crews install it, and outside engineers check it. In-house teams cover the electrical and mechanical work without subcontractors, installers include veterans with more than 20 years on conveyor, and the finished work is reviewed by independent third-party engineers and safety inspectors.
We stand behind it in writing. One-year warranty on installation quality, plus manufacturer warranties on the equipment.
We are still there after startup. Factory-trained technicians, locally stocked spare parts, and a 70-plus vehicle service fleet covering belt and slat replacement, drive service, and alignment. The team that installed it is the team that maintains it.
We can also work a new spiral into a line running older equipment, so a sanitary upgrade does not have to mean replacing everything around it.
Book an assessment with an HOJ engineer. You get a working session with someone who designs, installs, and services these systems, not a rep reading off a spec sheet.
Testimonials
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.
READY TO GET STARTED?
REACH OUT TO US TODAY
Whether it’s a project, product, repair or service, let’s chat to see if we can make your warehouse operations more efficient.